Cushioning is an important factor in insole manufacturing, but material softness alone does not determine product performance. Foam density, compression resistance, thickness, resilience, and layer construction all affect how a cushioned insole performs.
For insole manufacturers, the challenge is to balance cushioning, structural support, durability, and production cost. Different applications require different material combinations, making material selection and process control essential for consistent bulk production.
1. Key Performance Requirements for Cushioned Insoles
A cushioned insole should absorb impact while maintaining its intended shape under repeated loading. Manufacturers need to evaluate several properties when developing a product:
- Impact absorption: The ability of the material structure to absorb loading during use.
- Compression resistance: The ability to withstand repeated pressure without excessive permanent deformation.
- Resilience: The material’s ability to recover after compression.
- Pressure distribution: The ability of the insole structure to distribute loads across the contact area.
- Structural stability: The ability to maintain the intended shape and support characteristics.
These properties should be assessed together. A low-density foam may provide a soft initial feel but may not offer sufficient compression resistance for a product exposed to repeated loading.
2. Common Materials for Cushioned Insole Production
Material selection depends on the target application, required cushioning level, product thickness, and manufacturing process.
EVA Foam
EVA (ethylene-vinyl acetate) is widely used in cushioned insoles because of its low weight, flexibility, and adaptable foam properties.
Different EVA grades can provide varying levels of hardness, density, and resilience. This makes EVA suitable for sports insoles, everyday footwear insoles, and orthotic constructions.
Key specifications to evaluate include:
- Density and hardness
- Compression set and recovery
- Foam thickness and cell structure
- Flexibility and dimensional stability
EVA is also suitable for cutting, molding, and thermoforming processes, depending on its formulation and product design.
PU Foam
Polyurethane (PU) foam is commonly used where cushioning and resilience are important. Its properties vary according to formulation, density, and foam structure.
PU can be incorporated into full-length cushioning layers or selected zones within a multi-layer insole. Manufacturers should assess its compression behavior, durability, dimensional stability, and bonding compatibility before production.
Microcellular Urethane Materials
Microcellular urethane materials, including PORON® products, are used in localized cushioning applications.
They can be incorporated into heel pads, forefoot pads, and other pressure-sensitive areas. Their performance depends on material grade, thickness, and loading conditions.
For production projects, the selected grade should match the required compression and recovery characteristics rather than being chosen by brand name alone.
Latex Foam
Latex foam offers flexible cushioning and resilience. It can be used as a cushioning layer or combined with other materials in multi-layer constructions.
Before bulk production, manufacturers should evaluate its density, compression behavior, dimensional stability, and compatibility with adhesives and adjacent materials.
PE Foam and Supporting Materials
Polyethylene (PE) foam is available in different densities and firmness levels. Depending on the design, it can serve as a lightweight cushioning or structural layer.
TPU and other thermoplastic components may also be used to reinforce specific areas. These materials generally serve a supporting role rather than replacing the primary cushioning layer.
3. Structural Design of Cushioned Insoles
The final performance of an insole depends on how materials work together. Layer thickness, material placement, and support geometry should be considered during product development.
Multi-Layer Construction
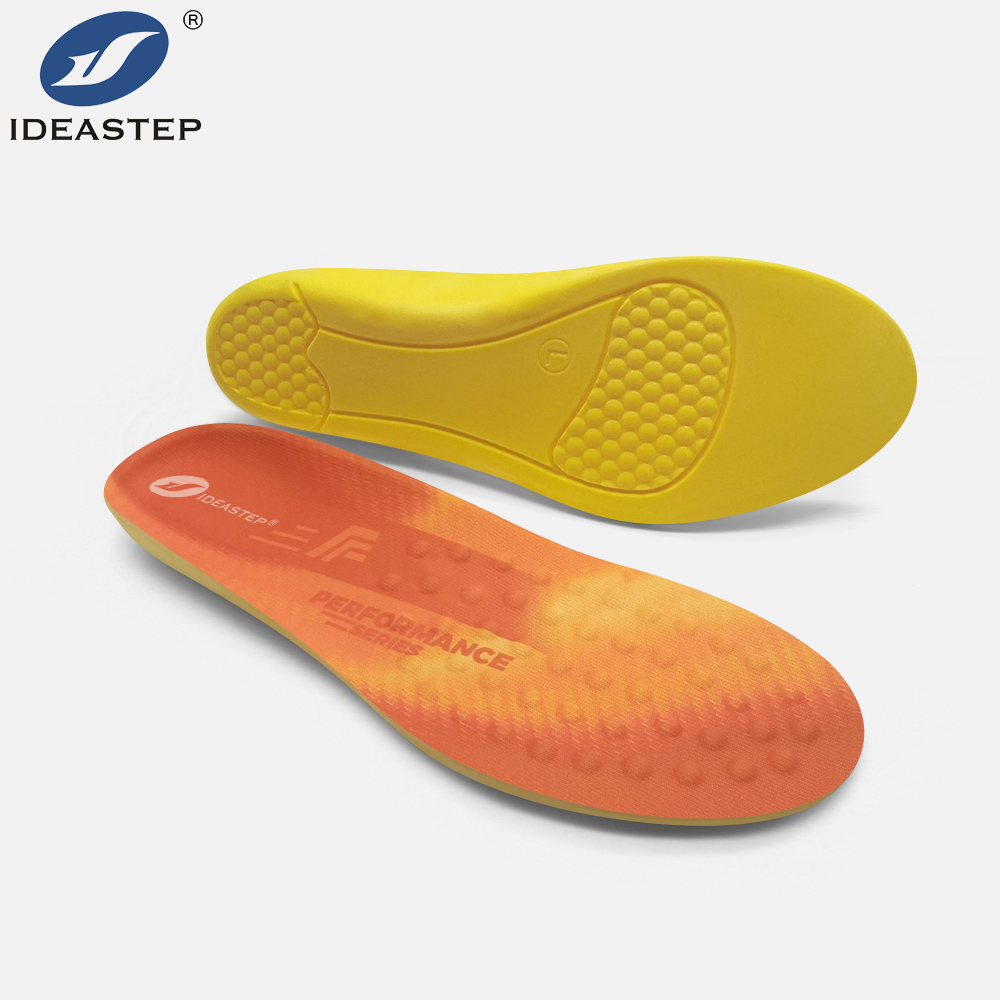
A typical multi-layer insole may include:
- Top cover: Fabric or textile selected for surface durability and moisture management.
- Cushioning layer: EVA, PU, or microcellular urethane for impact absorption.
- Support layer: A semi-rigid or reinforced component to maintain structural stability.
- Bottom layer: A material selected for bonding and compatibility with the footwear.
Not every product requires all four layers. The construction should match the intended application while avoiding unnecessary thickness, weight, and production cost.
Heel and Forefoot Cushioning
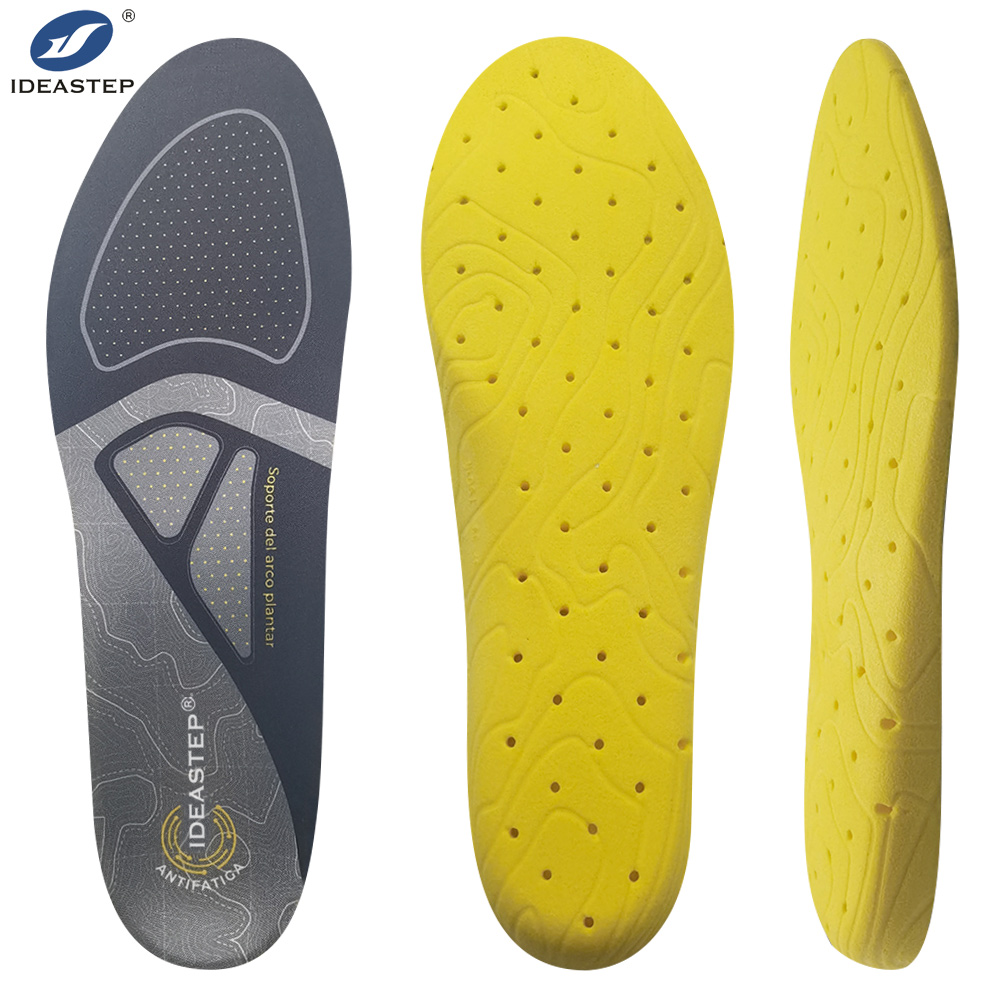
Heel and forefoot areas experience different loading conditions. Some designs therefore use localized cushioning to meet specific performance requirements.
Heel sections may require greater cushioning thickness or compression resistance, while forefoot sections often need to balance impact absorption with flexibility.
Material grade and thickness should be validated within the complete insole structure.
Arch and Midfoot Support
Cushioning and structural support serve different functions. In orthotic and functional insole designs, the arch and midfoot may require a shaped support layer or semi-rigid shell.
The foam layer must work with the support component without compromising the intended geometry. Manufacturers should evaluate material compression and structural deformation during prototype testing.
Thickness and Density Distribution
Some designs use uniform foam thickness, while others apply different thicknesses or densities across selected zones.
This approach allows manufacturers to adjust cushioning and flexibility within one product. However, transitions between materials should be controlled to avoid uneven surfaces, weak bonding areas, or inconsistent product dimensions.
4. Matching Materials to Different Insole Applications
Material combinations should be based on the technical requirements of each product line.
| Product Category | Common Material Options | Main Manufacturing Considerations |
|---|---|---|
| Sports insoles | EVA, PU, microcellular urethane | Impact absorption, resilience, flexibility |
| Work footwear insoles | EVA, PU, layered foam | Compression resistance, durability, thickness |
| Everyday cushioned insoles | EVA, PU, latex foam | Flexibility, cushioning consistency, cost |
| Orthotic insoles | EVA, PU, PORON®, support shells | Cushioning and structural support |
| Diabetic footwear insoles | Soft EVA, PU, specialized cushioning materials | Pressure distribution, material consistency, surface construction |
These are general material options rather than fixed formulas. Final specifications should account for product geometry, footwear construction, expected loading, and applicable requirements.
5. Manufacturing and Quality Control
Consistent cushioning requires control over incoming materials, processing conditions, and finished-product specifications.
Material Inspection
Incoming foam materials should be checked against approved specifications. Relevant properties include density, hardness, thickness, appearance, and batch consistency.
Compression and recovery characteristics should also be evaluated where they are part of the product requirements.
Cutting and Forming
Die cutting, CNC machining, molding, and thermoforming are common processes in insole production.
Cutting accuracy affects product dimensions and material utilization. For molded or shaped components, mold condition and forming parameters also influence repeatability.
Lamination and Bonding
Multi-layer constructions require reliable bonding between the top cover, foam, and support components.
Adhesive selection, surface preparation, bonding pressure, and curing conditions all affect bond strength. Production inspection should identify peeling, bubbles, uneven bonding, and edge separation.
Finished Product Inspection
Inspection criteria should be defined before mass production. Depending on the product, checks may include:
- Overall length, width, and thickness
- Material density and hardness
- Compression set and recovery
- Bonding strength between layers
- Shape consistency and surface defects
- Flexibility and durability under repeated loading
Approved samples, technical drawings, and inspection records provide a consistent reference for repeat orders.
6. Challenges in Bulk Cushioned Insole Production
Scaling production requires more than increasing output. Manufacturers must maintain material and product consistency across batches.
Material variation: Differences in foam density, hardness, and thickness can affect finished-product performance. Approved material specifications and batch records help control variation.
Compression performance: Initial softness does not necessarily indicate long-term performance. Compression set and recovery should be considered when selecting materials for repeated loading.
Bonding reliability: Multi-layer constructions introduce additional quality risks, especially when materials have different surface properties or adhesive requirements.
Production efficiency: Material thickness, cutting yield, scrap, labor, and processing time all influence unit cost. Material combinations should be evaluated for both performance and manufacturing efficiency.
Repeat-order consistency: Suppliers should maintain approved material grades, construction details, dimensions, and inspection standards across production batches.
7. Technical Specifications for Wholesale and OEM Orders
Clear specifications reduce misunderstandings during sampling and bulk production. Buyers and manufacturers should confirm the following before placing an order:
- Insole dimensions and size range
- Material types, grades, and thicknesses
- Target density and hardness, where applicable
- Layer structure and support components
- Top cover and surface finish
- Product application and performance requirements
- Logo, packaging, and private label details
- MOQ, sample lead time, and bulk production lead time
- Quality inspection criteria and approved sample standards
For custom projects, technical drawings and reference samples should be reviewed alongside material specifications. This helps ensure that mass production follows the approved construction.
8. Custom and OEM Cushioned Insole Production
Cushioned insoles can be developed with different foam grades, thicknesses, top covers, support structures, and surface finishes. These options allow manufacturers and brands to develop product lines for sports footwear, work shoes, everyday footwear, and specialized orthotic applications.
For OEM and private label projects, material specifications and product construction should be confirmed during sampling. Once the sample is approved, the same requirements should be maintained throughout bulk production.
For a new project, buyers can provide the intended application, preferred materials, size range, and estimated order quantity for technical evaluation and quotation.
Conclusion
Cushioned insole manufacturing depends on the right combination of material properties and structural design. EVA, PU, microcellular urethane, latex, and PE each offer different processing and performance characteristics.
For manufacturers and wholesale buyers, material selection should be supported by clear specifications, prototype testing, and consistent production controls. Density, compression behavior, layer bonding, and dimensional accuracy are key factors in maintaining product quality across bulk orders.
Related Insole Products: https://www.aideastep.com/product/ideastep-8639-breathable-pu-comfort-insoles-with-zoned-mesh-design/.